
Home
Products
Cellophane
Coated Waterproof Cellophane Paper
English Version
1. Product Introduction
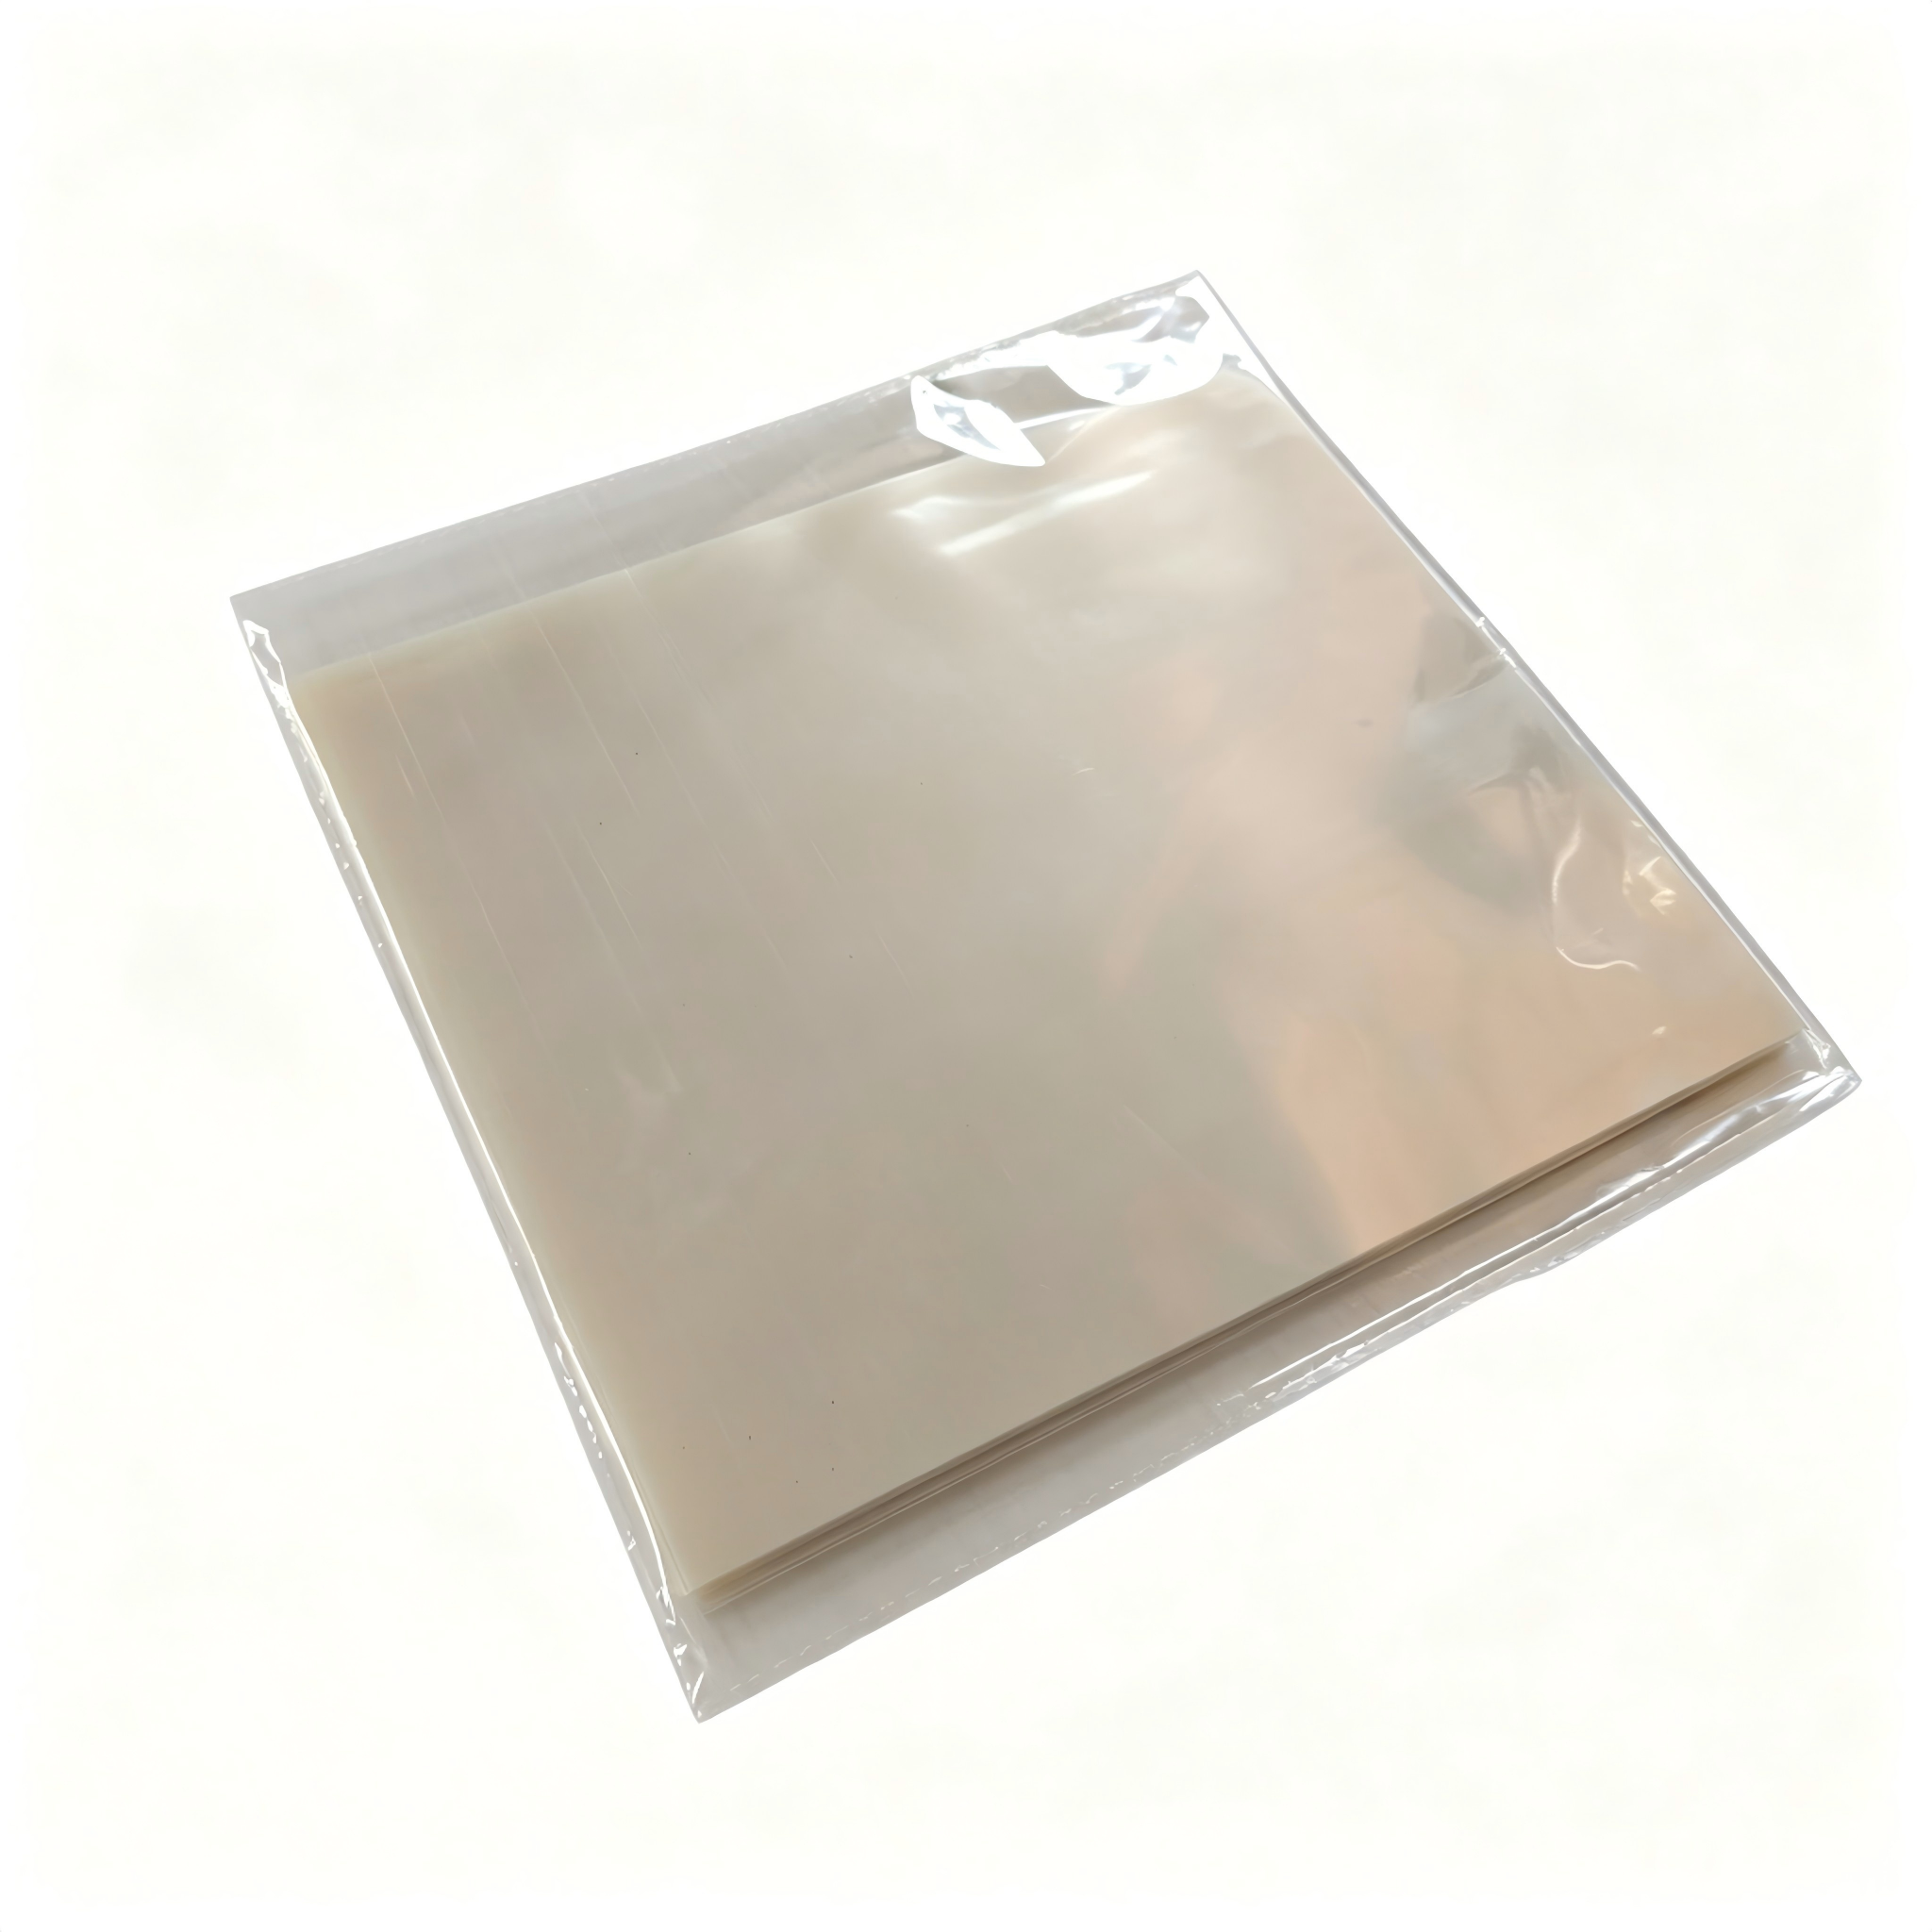
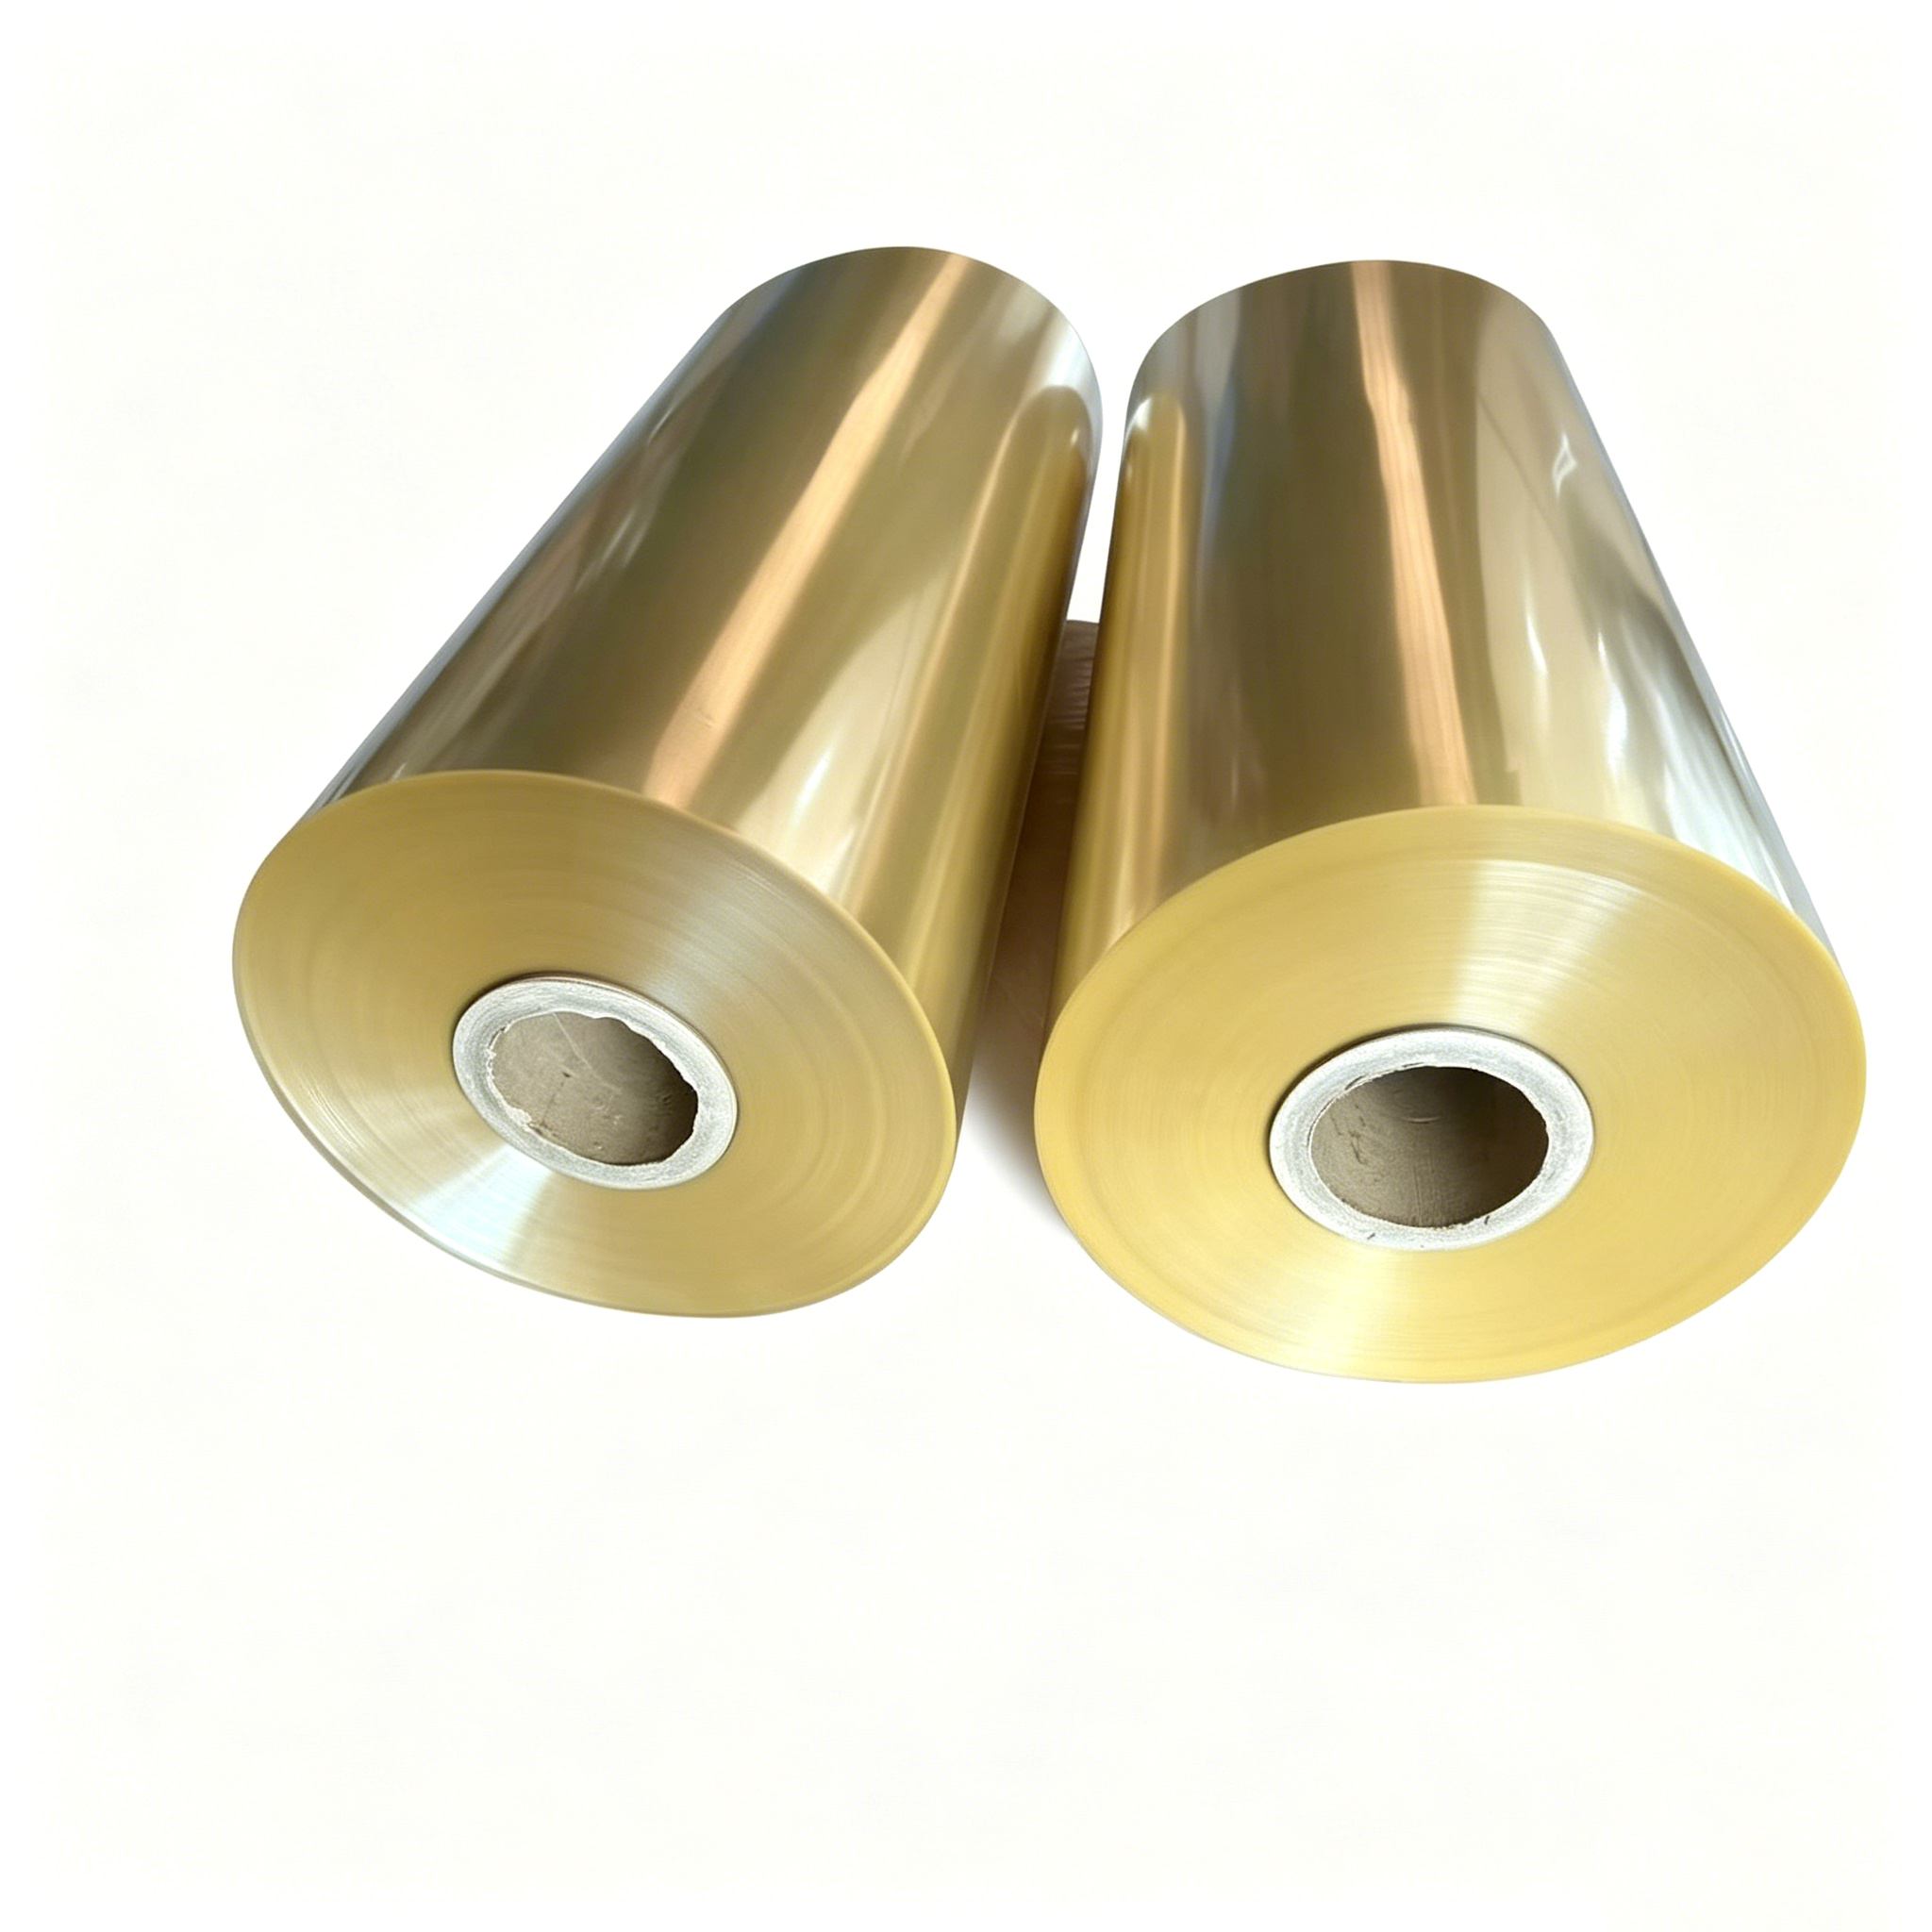
Coated Cellophane, professionally named Coated Waterproof Cellophane Paper, is an upgraded functional cellophane packaging material based on natural plant cellulose. Different from ordinary non-coated cellophane, this waterproof cellophane paper is treated with a professional food-safe coating process on the surface, forming a dense waterproof and moisture-proof protective layer. It perfectly retains the original advantages of cellophane such as high transparency, food-grade safety, air permeability and full biodegradability, while greatly improving water resistance, moisture resistance and surface strength. The coated waterproof structure effectively prevents water penetration, moisture absorption and deformation in humid environments. It is widely used for moisture-proof packaging of food, gifts, daily necessities and industrial products, especially suitable for products that require both breathable fresh-keeping and waterproof protection, serving as an ideal functional green packaging material for humid climate and long-distance transportation.
2. Product Features & Core Advantages
- Professional Coated Waterproof Treatment:Adopts advanced food-safe coating technology to form a uniform and dense waterproof film on the cellophane surface. It effectively resists water splashing, surface moisture and humid erosion, solving the defect that ordinary cellophane is easy to absorb water and get soft, greatly improving the product’s environmental adaptability.
- Breathable & Moisture-proof Dual Performance:While achieving surface waterproofing, it maintains uniform micro-air permeability inside the paper body. It blocks external liquid water and water vapor infiltration, and discharges internal excess moisture, realizing waterproof, breathable and mildew-proof triple effects to keep products dry and fresh.
- Food-grade Safety & Non-toxic:Both the base cellulose material and surface coating agent comply with international food contact safety standards, without fluorescent agents, plasticizers and harmful substances. It is non-toxic, odorless and harmless, safe for direct food packaging.
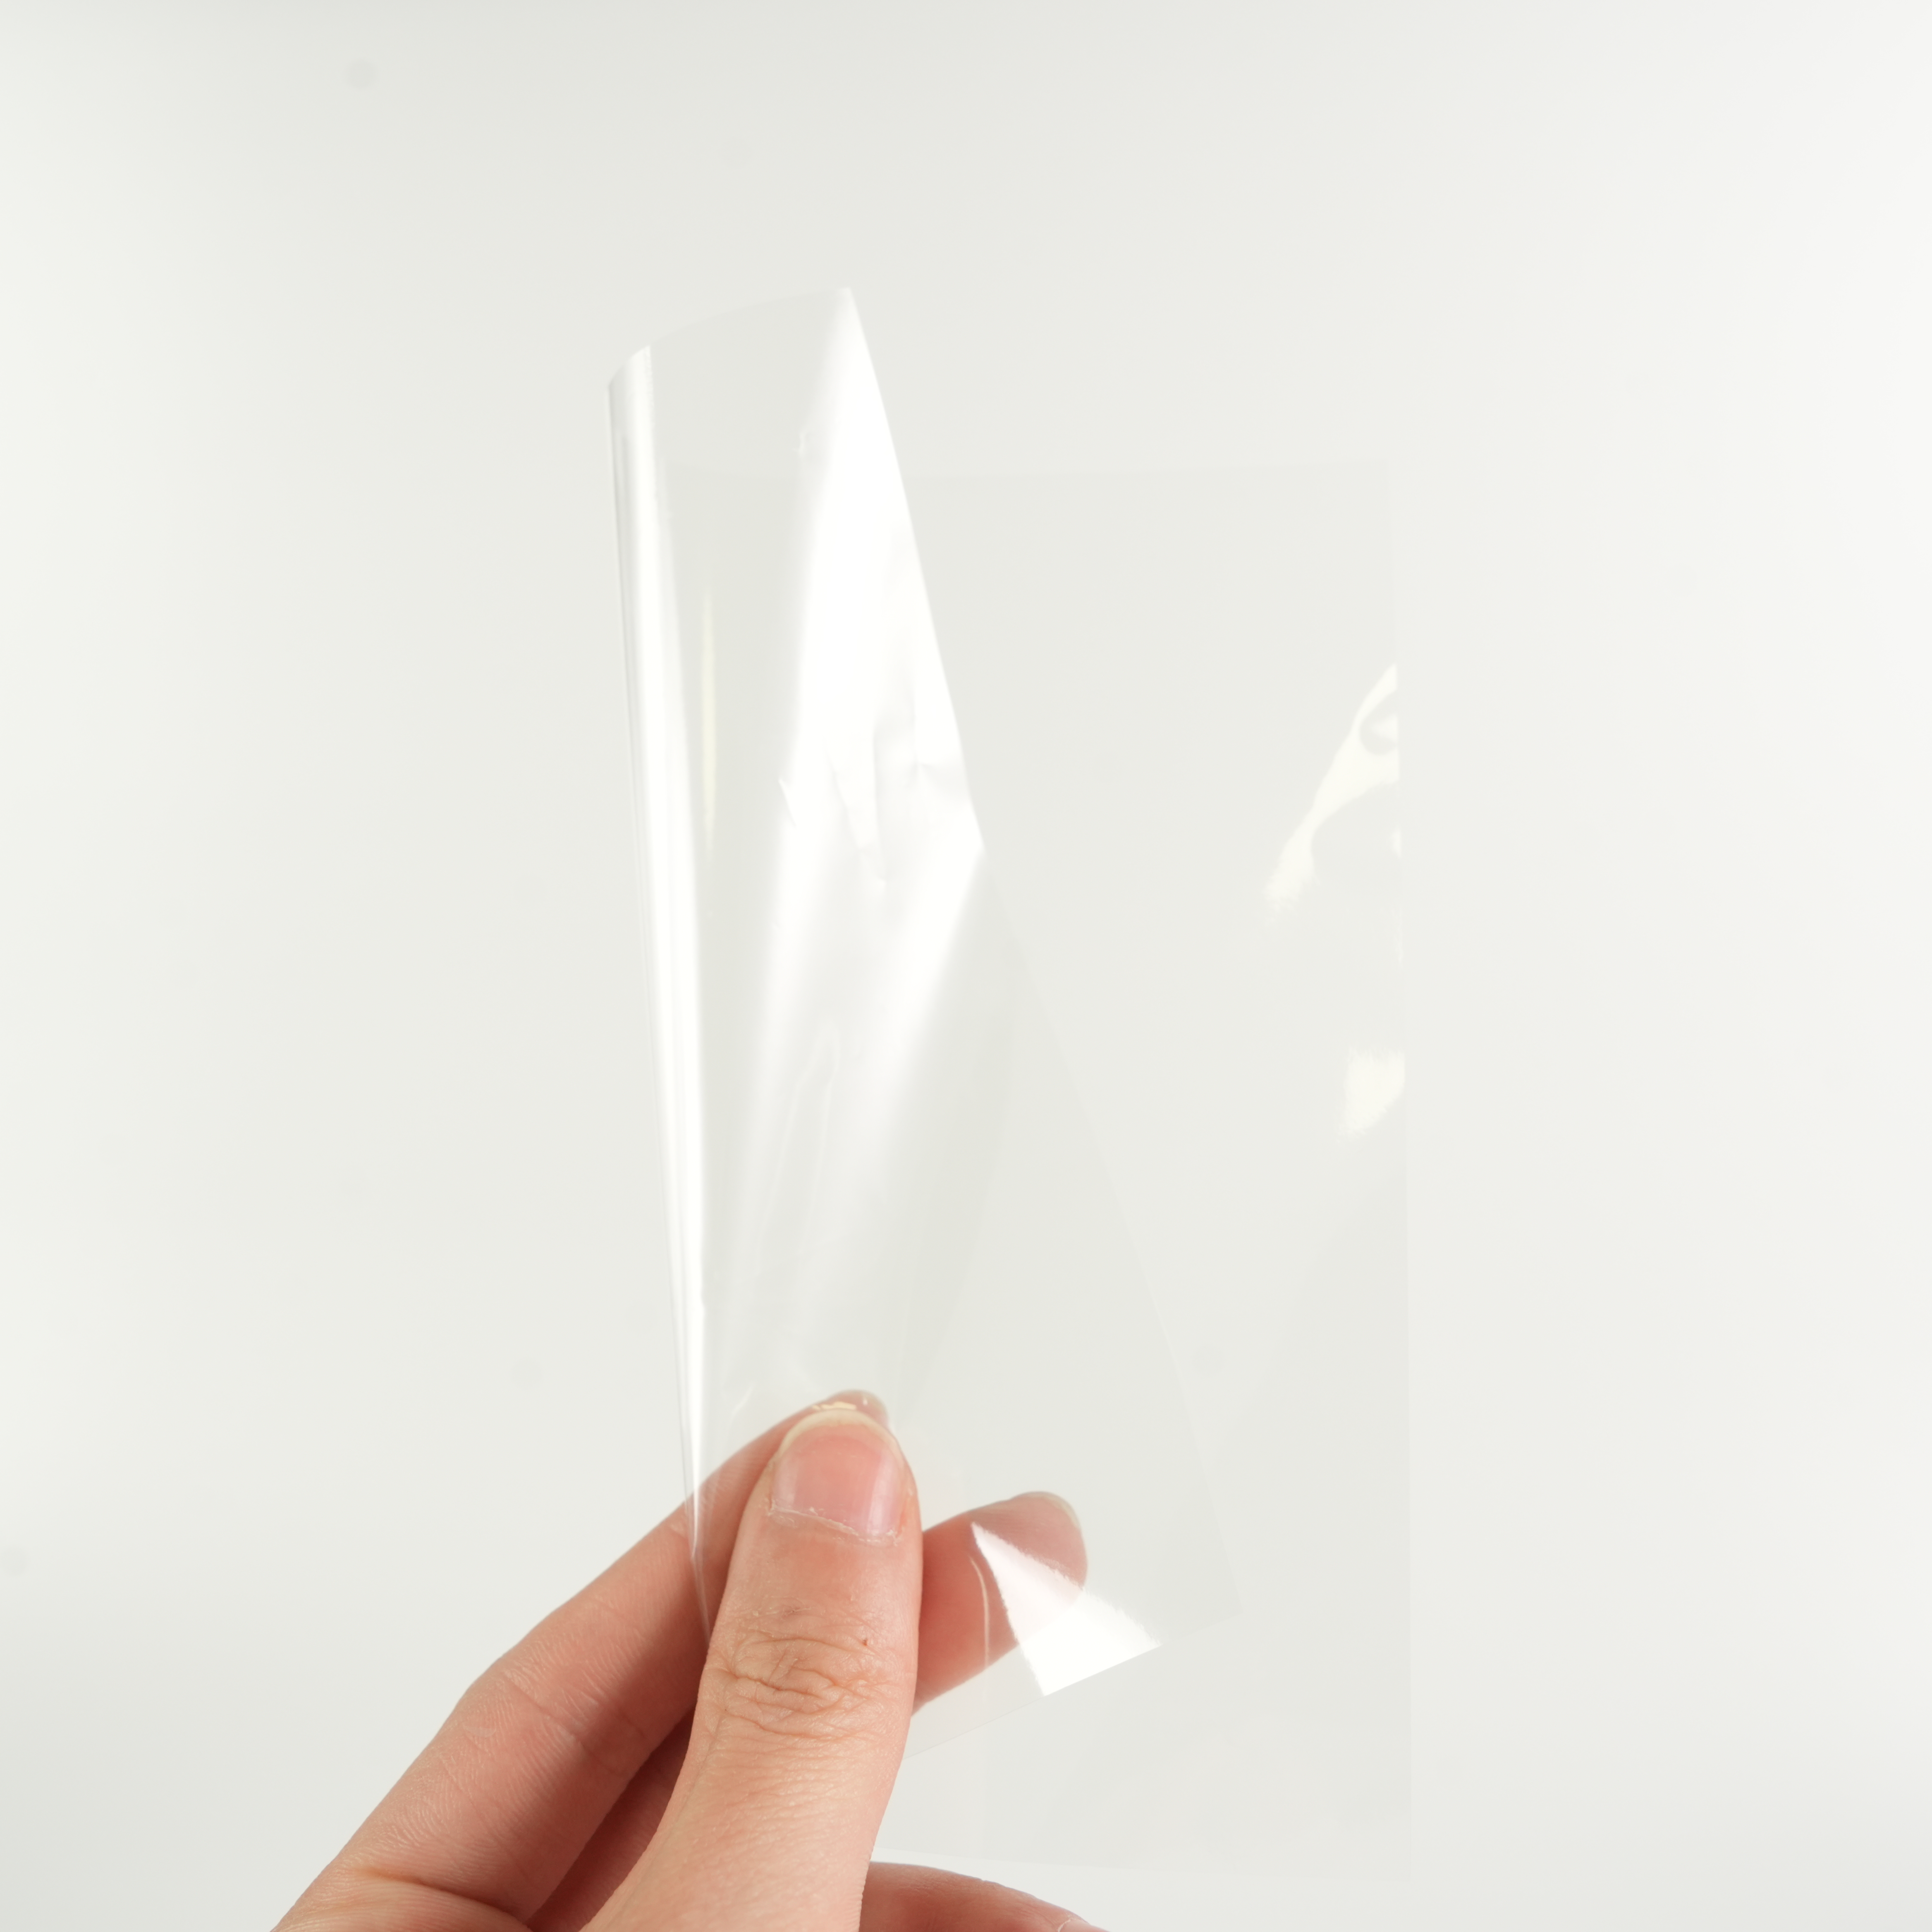
- High Transparency & Premium Appearance:The special coating layer is ultra-thin and high-transparent without fogging, maintaining the crystal clear texture and high-gloss surface of cellophane. It fully displays the appearance and texture of packaged goods without affecting the display grade.
- Enhanced Surface Toughness & Durability:The coating layer strengthens the surface structure of cellophane, improving tensile resistance, scratch resistance and abrasion resistance. The paper is not easy to crack, deform or wrinkle during packaging, transportation and storage, with more stable overall performance.
- 100% Biodegradable & Eco-friendly:The whole material including the coating layer is made of degradable environmental-friendly formula. It can be completely decomposed into carbon dioxide and water in natural compost and soil environment, zero microplastic residue, in line with global sustainable green packaging standards.
- Anti-static & Dust-proof:With excellent anti-static performance, it avoids dust and fine particle adsorption, keeping the packaging surface clean and tidy, suitable for high-standard food and precision product packaging.
- Customizable Size & Printing:Support customized thickness, size, sheet/roll type and brand logo, pattern and text printing. It can meet personalized waterproof packaging needs of different industries and brands.
3. Product Technical Specifications
- Product Name: Coated Cellophane / Coated Waterproof Cellophane Paper
- Base Material: Natural regenerated plant cellulose
- Surface Treatment: Food-grade waterproof degradable coating
- Thickness Range: 20μm – 100μm (customizable)
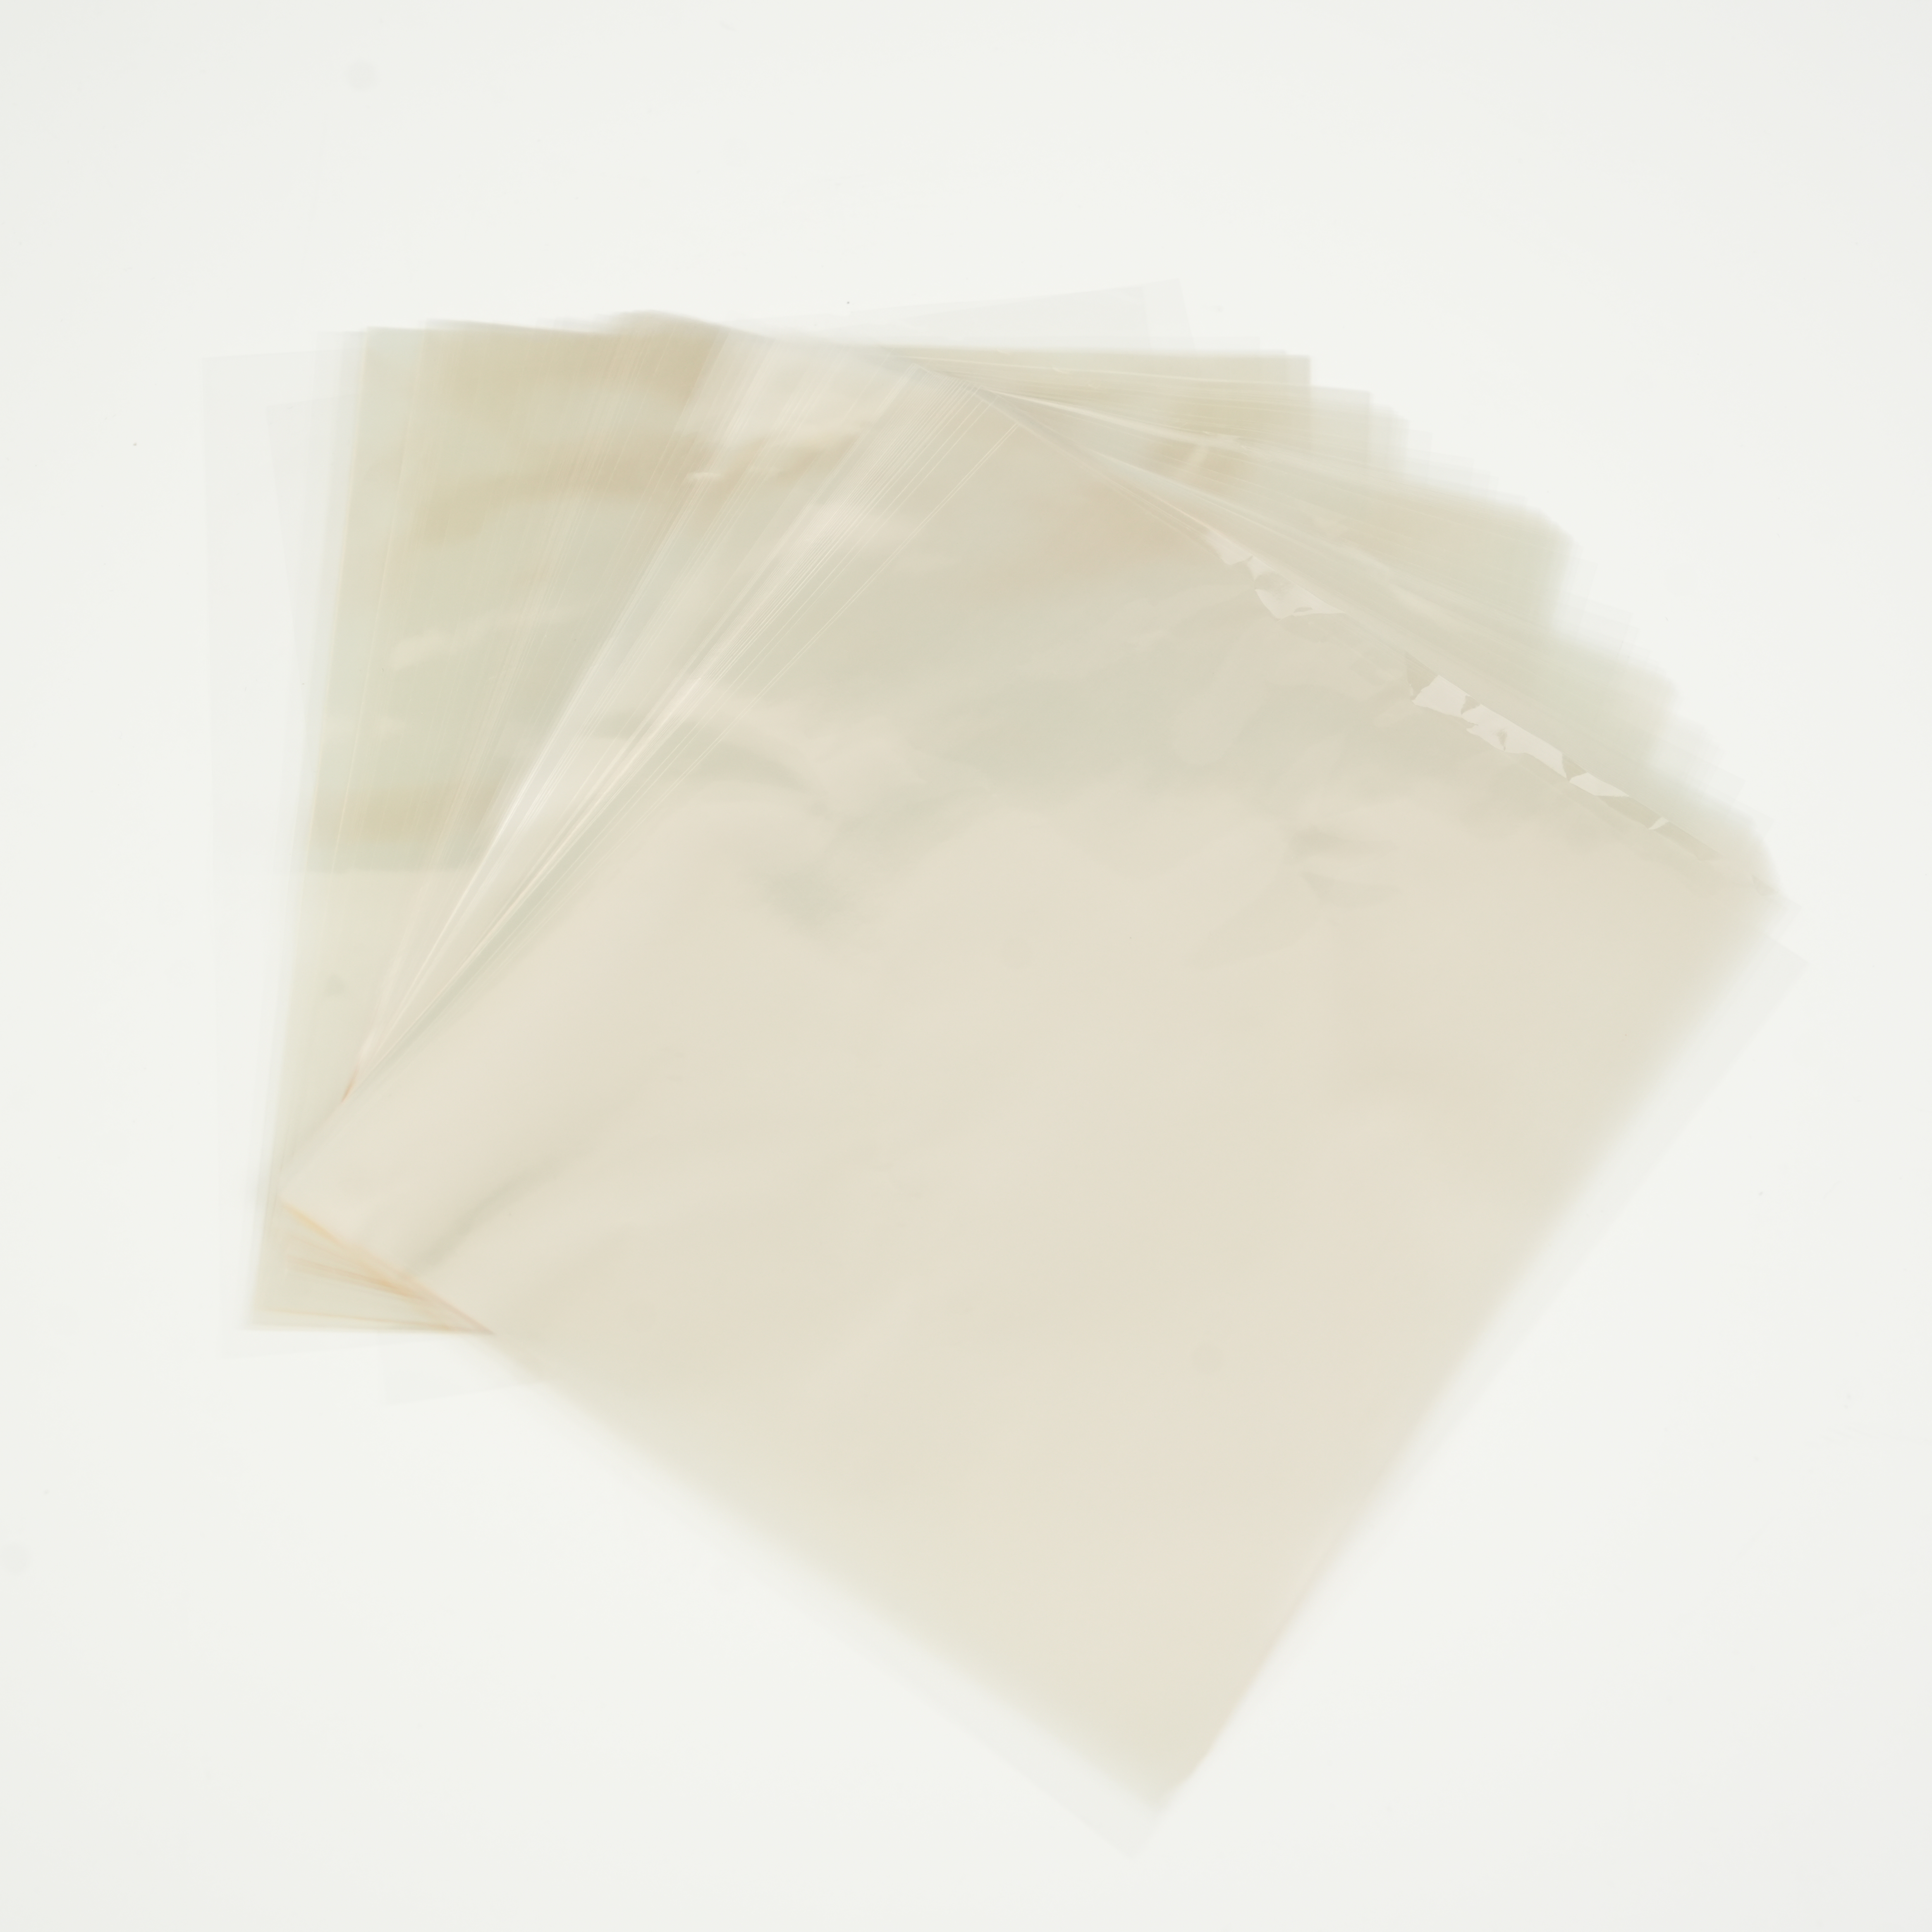
- Specification Type: Flat sheet / Roll type (customizable)
- Core Function: Waterproof, moisture-proof, breathable, fresh-keeping, dust-proof
- Transparency: Ultra-high transparent, no fog, high gloss
- Degradation Performance: 100% natural biodegradable, zero pollution
- Custom Service: Custom size, thickness, shape and printing
- MOQ: Flexible minimum order quantity, support sample and bulk orders
- Certification: International food-grade safety certification & biodegradation certification
4. Application Scope
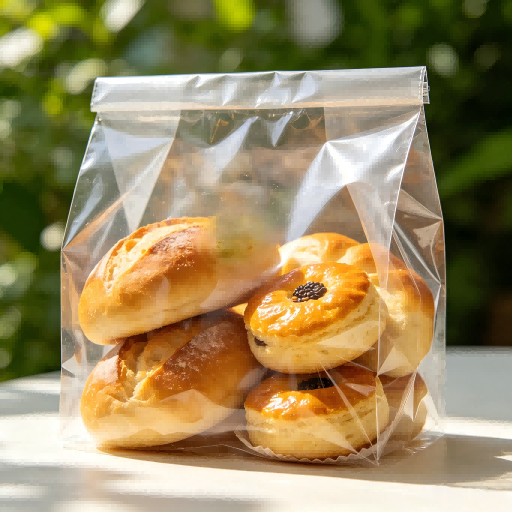
- Humid Environment Food Packaging: Moisture-proof packaging for candies, chocolates, pastries, dried fruits and nuts, suitable for long-distance transportation and humid area sales.
- Flower & Gift Waterproof Packaging: Waterproof and fresh-keeping wrapping for bouquets, holiday gifts and crafts, preventing moisture damage during transportation.
- Daily Necessities Packaging: Waterproof and dust-proof protective packaging for soap, cosmetics, toys and household products.
- Industrial Moisture-proof Protection: Moisture-proof isolation packaging for electronic accessories, hardware parts and precision stationery, adapting to complex storage and transportation environments.
5. Factory & Service Advantages
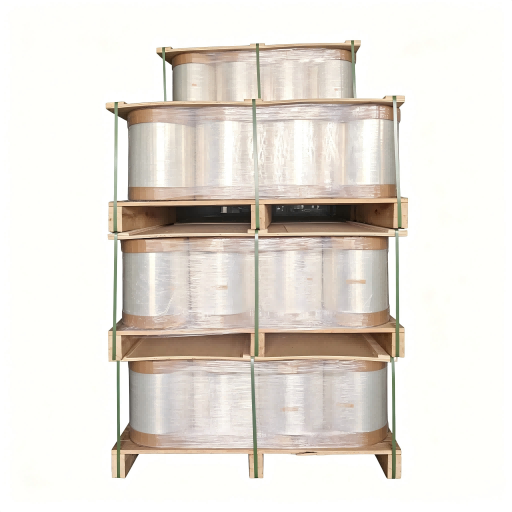
We are a professional manufacturer specializing in coated waterproof cellophane paper. We adopt imported natural cellulose raw materials and eco-friendly food-grade waterproof coating technology. All products feature stable waterproof performance, high transparency and full biodegradability. Strict quality inspection is implemented for each production procedure to ensure food safety and stable physical properties. We support customized sizes, specifications and brand printing services. With reliable quality and fast delivery, our coated cellophane products are exported to global markets, providing professional waterproof and breathable green packaging solutions for worldwide customers.